Description
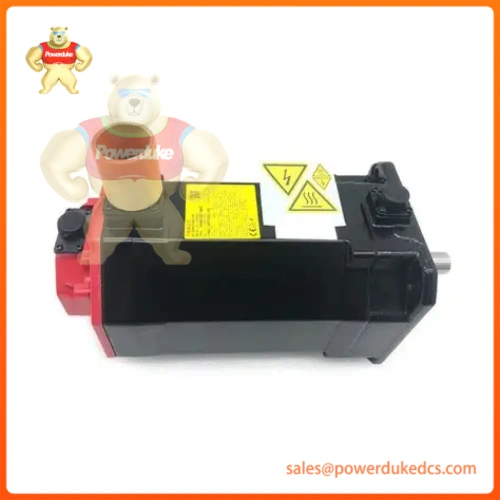
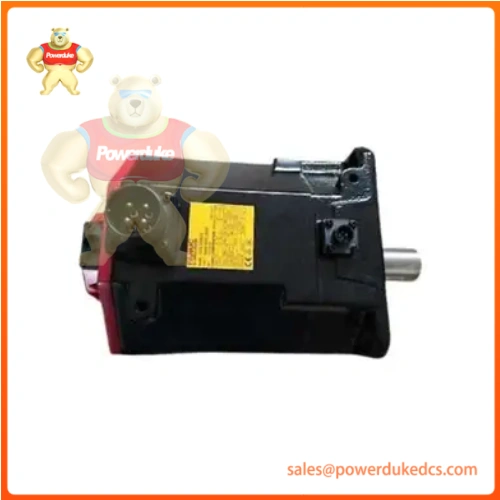
The A06B-0272-B605 (often designated with a suffix like #S000) is a high-performance Alpha iS series AC Servo Motor (specifically model \alpha iS 30/4000 or \alpha iS 40/4000) manufactured by Fanuc.
This motor is widely deployed on heavy-duty CNC machine axes (such as milling machines, large turning centers, and boring mills) that require a combination of high torque output, rapid acceleration, and precise positioning capabilities under rigorous cutting loads.
Technical Specifications
The model suffix (-B605) defines the physical configuration parameters of the motor output shaft, feedback system, and internal mechanical safety options:
| Parameter | Specification / Value |
| Brand | Fanuc |
| Part Number | A06B-0272-B605 |
| Motor Series | \alpha iS (Alpha iS Series) |
| Base Model Reference | Model \alpha iS 30/4000 or \alpha iS 40/4000 |
| Shaft Type | Tapered Shaft with a Keyway |
| Brake Configuration | Integrated 24 V DC Holding Brake |
| Feedback Sensor | Fanuc A860-2010-T341 (\alpha iAR128 absolute pulse coder) |
| Maximum Rated Speed | 4,000 RPM |
| Cooling Method | Natural conduction / totally enclosed structure |
Field Application and System Integration Notes
Tapered Shaft vs. Direct Couplings
The -B605 hardware identifier designates a tapered shaft profile machined with a standard locking keyway.
- Mechanical Interface: This configuration is highly specialized for machine builders who utilize precise, taper-fit timing belt pulleys or direct taper-lock couplings to completely eradicate mechanical backlash.
- Installation Warning: When mounting or removing pulleys or gears onto the shaft, never strike the end of the shaft with a hammer. Structural shock loads bypass the main casing and directly fracture the glass matrix disc housed inside the rear pulse coder, rendering the feedback loop useless.
24 V DC Brake Operation and Safe Interlocking
This motor includes an internal electromagnetic spring-set holding brake used to secure vertical or heavy sloped machine axes (e.g., a CNC Z-axis headstock) against gravitational dropping when the machine loses power.
- Holding Only: The internal brake is structurally rated only as a holding device, not a dynamic friction brake. Engaging the brake while the motor is spinning at high speed will prematurely wear out the friction lining and ruin the torque profile of the assembly.
- Sequencing: Ensure your CNC safety PLC or drive amplifier properly sequences the 24 V DC supply to release the brake prior to enabling the servo velocity loop, preventing the motor from driving against its own mechanical lock.
Pulse Coder Coordination
The motor relies on an absolute A860-2010-T341 encoder to track location.
- If swapping a damaged motor with a new surplus unit, you must re-verify the absolute position reference on the CNC control system. Because the new motor shaft orientation will be micro-aligned differently from the original unit, grid shifts or axis reference point calibrations (Fanuc Parameter 1815) are required to restore machine coordinate accuracy and prevent physical overtravel crashes.
Commercial and Procurement Data
- Product Condition: New Original (Factory Stock) or Refurbished/Tested Exchange Core (fully pressure washed, statically wound-tested, insulation breakdown Megger tested, and verified on a live Fanuc test stand).
- Standard Warranty: 12-month comprehensive warranty covering physical defects.
- Estimated Lead Time: Typically leaves warehouse facilities within 1 to 3 business days. Priority air-freight options are available for acute field breakdown recovery.
- Pricing Notice: Total procurement costs vary based on whether you are utilizing a Core Exchange program (returning the defective motor for a credit rebate). Contact our CNC drive and motor components desk for an itemized commercial proposal.
FANUC A06B-6290-H207 Alpha i Servo Amplifier Module (SVM2-40/40iF) Fanuc A860-2010-T341 Alpha i-A 128 Pulse Coder (Encoder) Fanuc A860-2060-T321 Pulse Coder \alpha iAR128 Encoder