Description
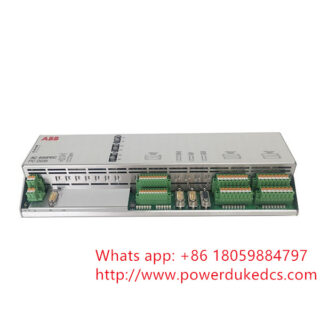
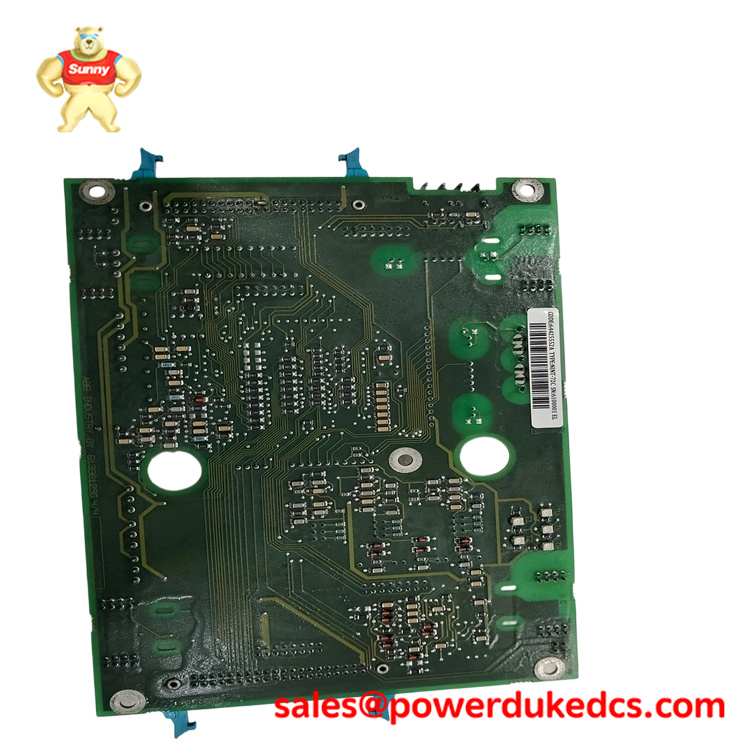
ABB NU8976A99 (HIER466665R0099) is a high-performance analog input/output processor module for ABB industrial control systems. It provides precise signal processing for field devices in DCS and PLC environments. This module addresses the need for reliable analog data handling in automation by offering high-resolution conversion and robust isolation.
Product Overview
The NU8976A99 HIER466665R0099 processes multiple analog channels with 16-bit resolution, supporting 0-20 mA and 0-10 V signals for sensors and actuators. Associated with part HIER466665R0099, it integrates into ABB System 800xA platforms for real-time control and monitoring. The ABB NU8976A99 features advanced diagnostics and fault tolerance, ensuring continuous operation in demanding process applications while minimizing wiring complexity.
Technical Specifications
- Brand: ABB
- Model:NU8976A99 HIER466665R0099
- Warranty: One Year
- Condition: 100% New & Original
- Input/Output: 16 analog channels; 0-20 mA / 0-10 V; 24 VDC logic
- Operating Temp: -40°C to +85°C
- Communication: Modbus RTU/TCP, Profibus, Ethernet
- Dimensions/Weight: 65 x 90 x 110 mm; 0.3 kg
- Power Supply: 24 VDC
- Isolation: 1500 Vrms channel-to-channel

Key Features & Benefits
- High-Resolution Processing: 16-bit A/D and D/A conversion delivers precise measurements (±0.1% accuracy), enabling fine control in continuous processes.
- IP67 Environmental Protection: Sealed design withstands dust, moisture, and vibration, supporting field-mount installations.
- Multi-Protocol Support: Seamless integration with Modbus and Profibus networks facilitates upgrades in mixed legacy/modern systems.
Application Scenarios
- Chemical Processing: Monitors pH and flow transmitters for batch reactions, providing stable control signals.
- Water Treatment: Interfaces level and pressure sensors in pump stations for automated dosing.
- Power Generation: Handles temperature inputs for boiler controls, ensuring efficient steam management.
Frequently Asked Questions (FAQ)
- Q: What is the primary function of the NU8976A99?
A: It serves as an analog I/O processor for ABB DCS systems, managing high-precision field signal conversion. - Q: Is NU8976A99 compatible with legacy systems?
A: Yes, it supports Modbus RTU/TCP and Profibus for integration with older ABB controllers and third-party PLCs. -
- Enjoy Chat and Email support in below
Email: [email protected]
- Enjoy Chat and Email support in below